Silicone-coated nylon is a nylon base cloth carrying a crosslinked silicone elastomer layer instead of the polyurethane coating almost every other waterproof bag uses. The honest answer to why anyone pays for it is not that it blocks more water — on a flat hydrostatic test it usually blocks less — but that it keeps doing what it did on day one for far longer. It stays soft at temperatures where polyurethane goes board-stiff, it does not hydrolyse into a tacky film in a humid warehouse, it resists ultraviolet yellowing, and it gives a dry, slippery hand that reads as expensive the moment a customer picks the bag up. Those four properties are why it sits at the top of the lightweight and premium end of the market.
This guide covers what the coating physically is and how it differs from the silicone finishes suppliers also call silicone, why hand feel is a measurable property rather than marketing, the glass-transition numbers behind cold-weather performance, why hydrolysis is a two-to-five-year commercial risk rather than a laboratory curiosity, how silicone compares with polyurethane and TPU film, how to choose coating weight in grams per square metre, where silicone actively fights the sewing room and the print shop, what the water column figure hides, the tear-versus-abrasion trade-off that decides whether it belongs on your product at all, and what it costs. MOQ 500 pieces per style, sampling in 6–10 working days, bulk in 35–50 days, FOB Xiamen: these are the working terms at QUANZHOU JUNYUAN BAGS, custom waterproof bag production since 2014 in a 4,950 m² SGS-verified facility.
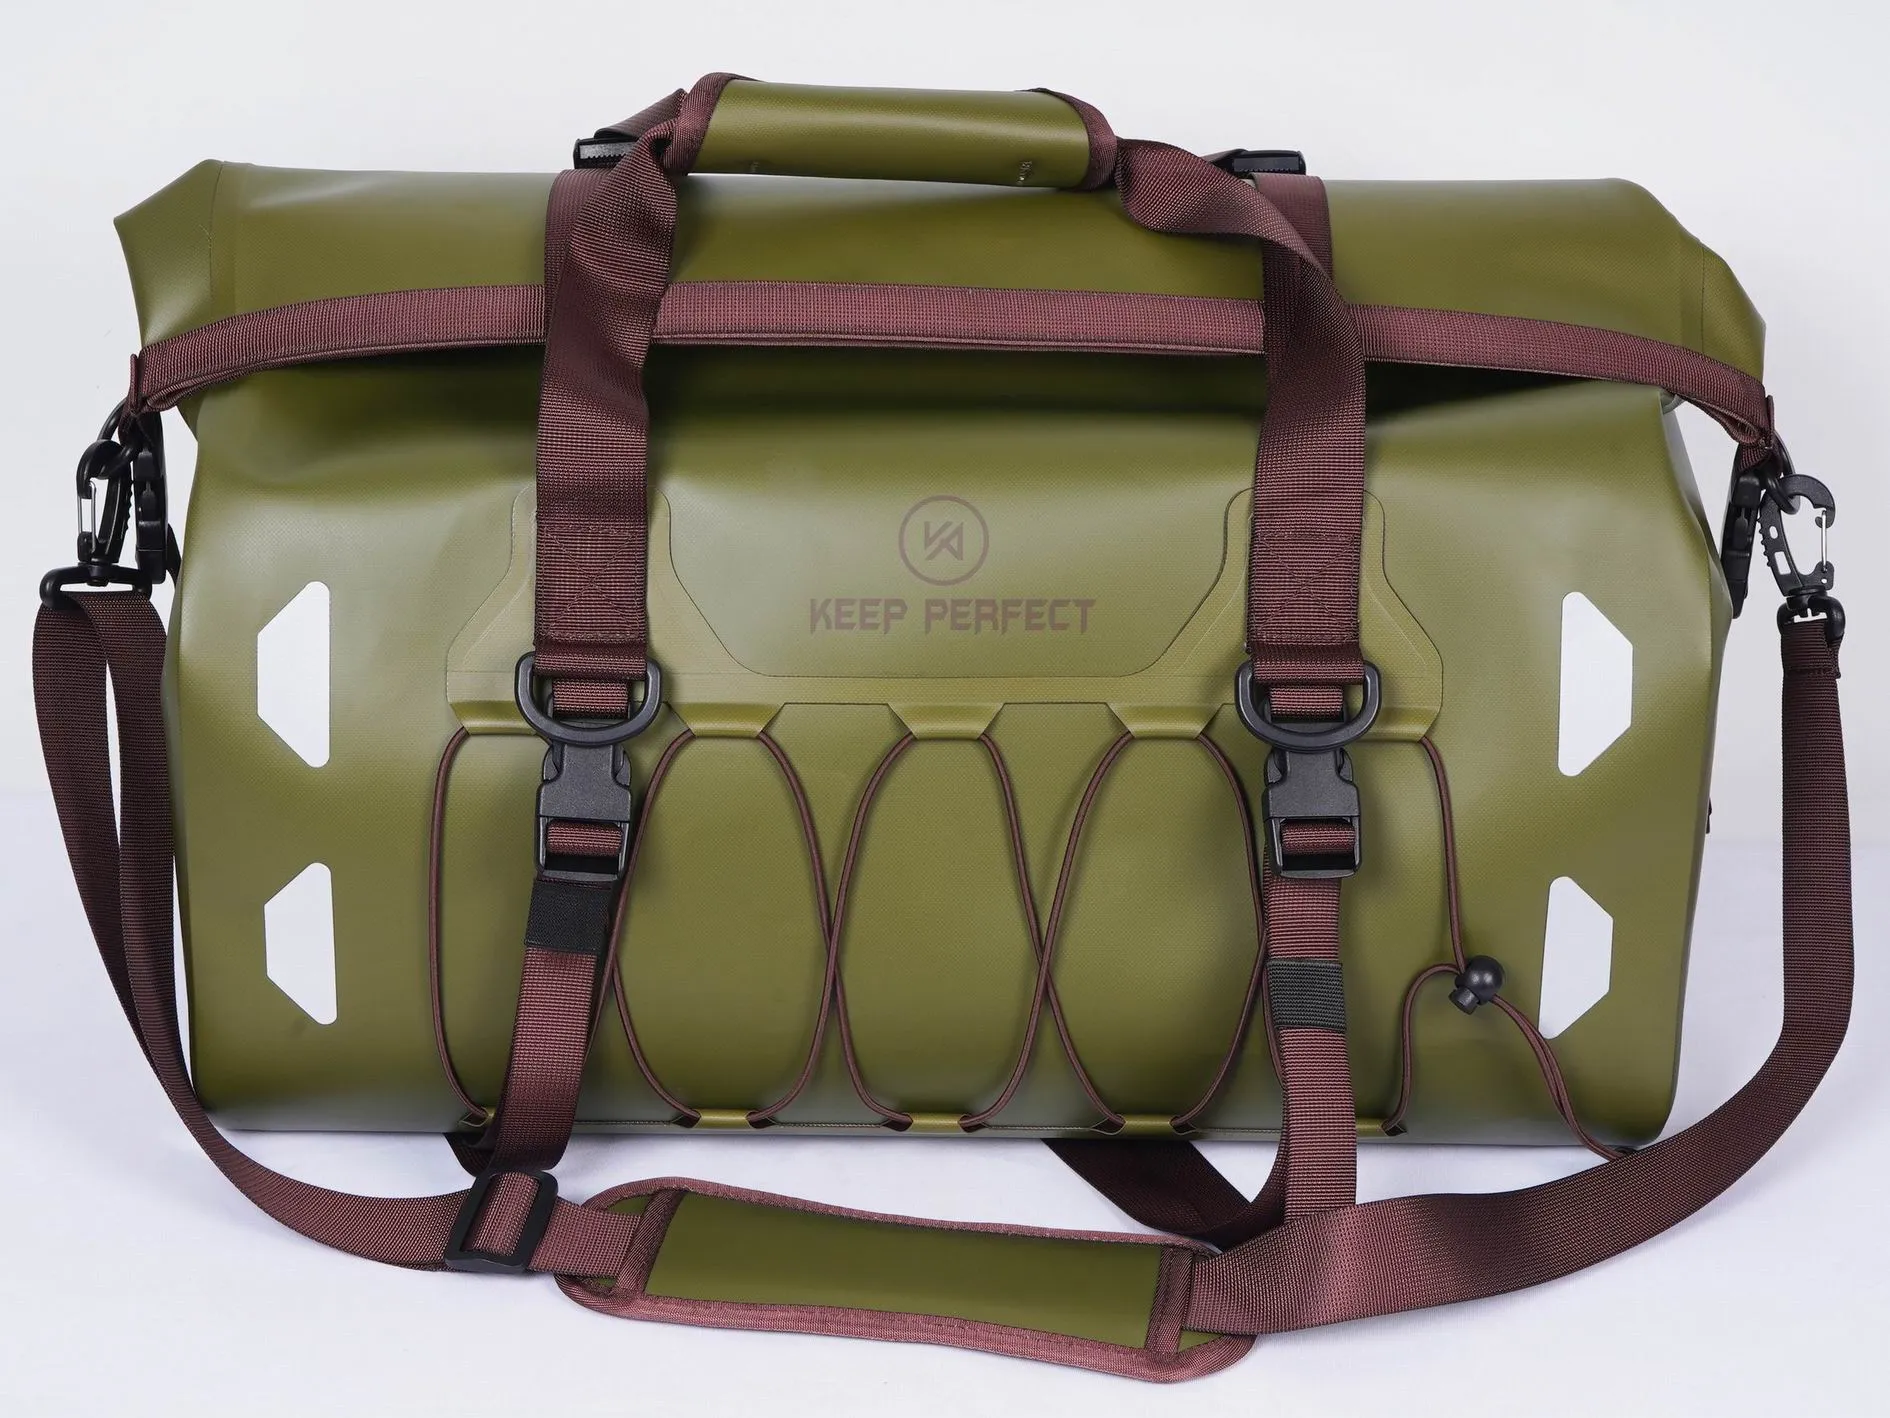
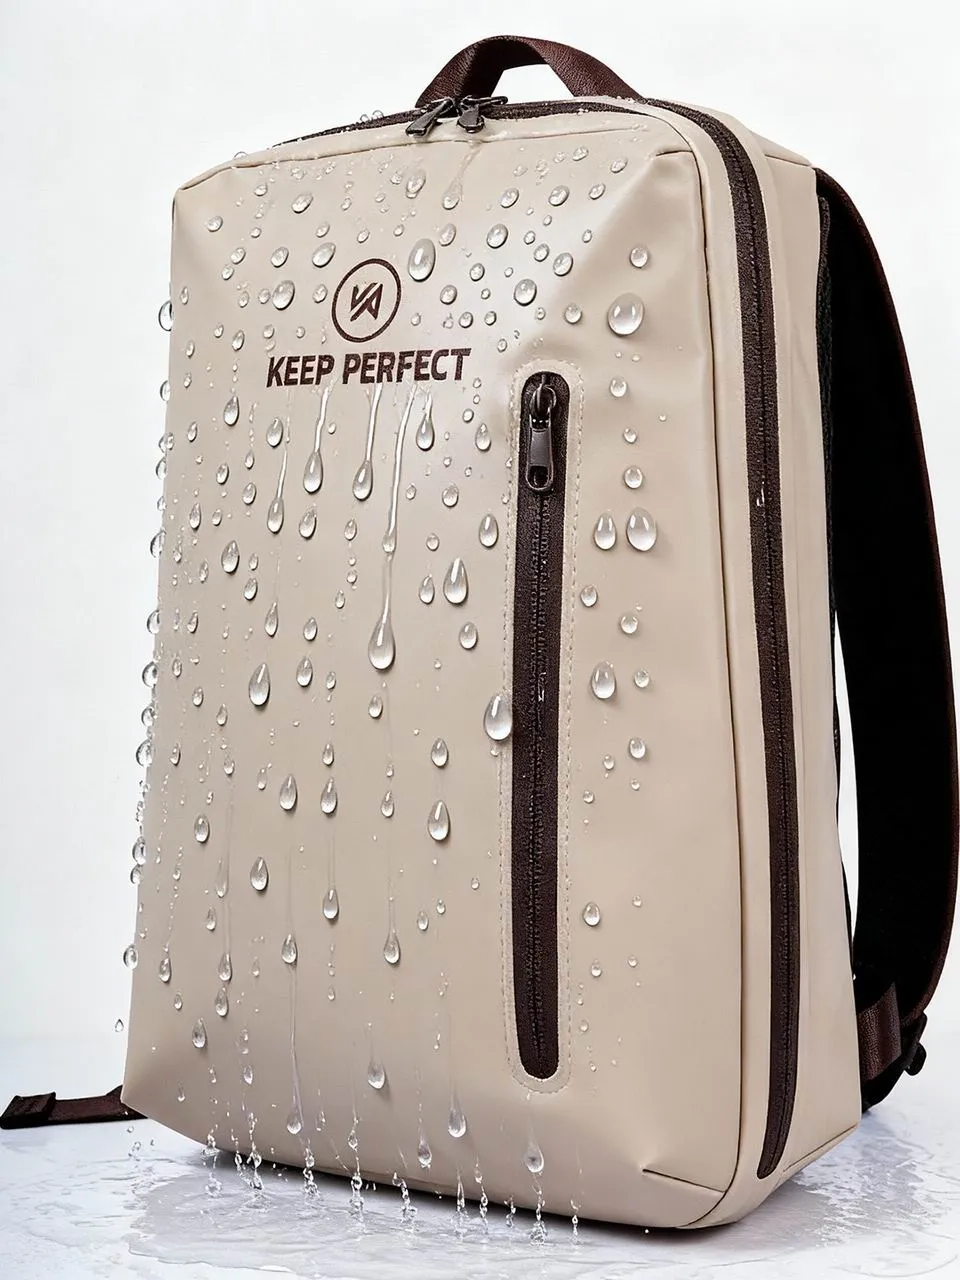
What silicone-coated nylon actually is
Most buyers meet silicone-coated nylon through a swatch and a price, and judge it as a nicer version of the polyurethane cloth they already buy. That is the wrong frame, because the two systems are chemically and mechanically different in ways that change how the bag must be built. A genuine silicone coating is a polydimethylsiloxane elastomer applied as a liquid, then crosslinked in place at roughly 150 to 180 degrees Celsius into a thermoset rubber. Once cured it does not melt, does not re-flow, and cannot be heat sealed. Everything downstream of that single fact — seam construction, printing, repairability — follows from it, and it is the reason so-called welded silnylon dry bags are rare and usually something else. As premium waterproof material it earns its position on longevity and feel rather than on headline numbers.
The base cloth underneath is almost always nylon 6 or nylon 6.6, usually a ripstop, and the denier range splits by application. Ultralight shells use 20 to 70 denier. General bag programmes use 210 to 420 denier where some abrasion resistance is needed. Ripstop matters more here than in polyurethane-coated cloth: because the silicone layer is soft and contributes relatively little to puncture and tear resistance, the reinforcement grid has to do that work, and a plain weave at the same denier performs noticeably worse.
The word silicone is then used loosely in quotations, and this is where specifications go wrong. There are three different things being sold under it. A true elastomer coating at 10 to 35 grams per square metre per side is a waterproof layer. A hydrophobic silicone finish at 2 to 5 grams per square metre is a handle modifier and water shedder applied on top of, or instead of, a real barrier, and it will not hold a water column on its own. And a silicone-polyurethane hybrid puts silicone on the face for feel and water shedding while leaving a polyurethane layer on the back so the fabric can still be welded.
- Ask for the dry add-on weight in grams per square metre, per side. A supplier quoting a finish will not be able to give you a meaningful number.
- Ask whether the fabric can be heat sealed or radio frequency welded. If yes, the sealing layer is polyurethane or TPU, not silicone.
- Ask which cure chemistry is used, addition cure with a platinum catalyst or condensation cure with a tin catalyst, because residual catalyst affects storage stability.
- Ask what the base cloth is: denier, weave type, ripstop grid spacing, and whether the yarn is nylon 6 or 6.6.
For background on where silicone sits relative to the other waterproof chemistries offered on the same production lines, our guide to DWR, PU and silicone coatings sets out the whole family, and the lamination routes that produce hybrid constructions are covered in our review of waterproof fabric lamination techniques.
Why the hand feel difference is not cosmetic
Hand feel is the first thing a retail customer notices and the last thing a specification mentions, which is odd, because it is both measurable and cheap to control. Two properties drive it. Surface friction: a cured silicone face has a coefficient of friction in the region of 0.2 to 0.3, against roughly 0.5 to 0.8 for a typical polyurethane face, and that is the difference between a shell that slides over a jacket and one that drags on it. Bending stiffness: silicone stays elastomeric at room temperature because its glass transition sits far below it, so it adds far less stiffness per gram of coating than polyurethane does.
That second point has a direct commercial consequence. Because the coating does not stiffen the cloth, a silicone-coated shell can be built from a much lighter base fabric and still feel substantial, and it compresses into a smaller packed volume because the plies slide over each other rather than gripping. On a mid-sized pack the shell panel weight can drop by 200 to 350 grams against a comparable polyurethane-coated build, and packed volume drops with it. For travel and ultralight programmes where the customer weighs the empty bag before buying, that is the entire pitch.
There is a real downside to a slippery face that nobody puts in a tech pack. Silicone-coated bags slide off a shoulder, slide across a car seat, and work loose from a compression strap in a way that polyurethane ones do not. Strap webbing with a silicone finish grips poorly against itself. Designers who have not handled the material before usually discover this at the first field test, and the fix is normally a hardware change rather than a material change: a grippier webbing, a different buckle geometry, or a silicone-free patch at the contact point.
None of this means silicone is universally more pleasant. Some buyers dislike the slightly dry, dusty feel and prefer the rubbery grip of polyurethane, and in a work or tool context that grip is genuinely safer. The point is that hand feel is a specified property with a number attached, not a matter of taste that has to be accepted as delivered.
Low-temperature flexibility: where polyurethane goes stiff
Every polymer has a glass transition temperature, the point below which its molecular chains stop moving freely and the material stops behaving like a rubber and starts behaving like a rigid solid. Silicone has one of the lowest glass transitions of any commercial polymer, around minus 120 degrees Celsius, which is why it is still flexible in conditions no bag will ever see. Polyurethane coatings sit far closer to their transition at ambient temperature, and most become noticeably stiff somewhere between minus 15 and minus 30 degrees Celsius, with the exact figure depending on the ratio of hard to soft segments in the formulation.
The practical consequence is not that the fabric tears at low temperature — nylon and polyester base cloths are fine — but that the coating cracks at the places the bag folds. A roll-top closure folded at minus 15 degrees, a lid folded shut on a frozen tailgate, a dry bag rolled up in a cold garage: these are the failures, and they present as a white crazed line along the fold that customers report as the bag splitting. The coating has not separated from the cloth and the cloth is undamaged; the surface film has exceeded what it could flex at that temperature.
| Material | Glass transition or brittle point | Behaviour at minus 20 °C | Where it fails in service |
|---|---|---|---|
| Silicone-coated nylon | Around minus 120 °C | Fully flexible, unchanged hand | Rarely cold-limited; fails on abrasion first |
| Polyether TPU film | Minus 45 to minus 55 °C | Flexible with slight stiffening | Good; the safe choice for welded cold-duty product |
| Polyester TPU film | Minus 30 to minus 40 °C | Stiffening noticeable under load | Acceptable down to about minus 20 °C |
| Polyurethane coating | Minus 15 to minus 30 °C | Boardy; crazes at tight folds | Roll-top creases, lid folds, webbing attachment points |
| Plasticised PVC | Minus 10 to minus 25 °C | Cracks on impact or sharp fold | Anywhere it is folded or struck while cold |
The test that captures this properly is a cold bend followed by a water column retest, not a cold bend alone. Condition the specimen at the target temperature for at least four hours, fold it around a specified mandrel at that temperature, let it return to ambient, then re-run the hydrostatic test on the folded region. A coating that passes flat and fails folded is exactly the failure mode described above, and a supplier quoting only a flat cold-bend result has not tested for it. Our companion article on cold and heat resistance in waterproof materials covers the wider temperature picture including the hot end.
Hydrolysis: a two-to-five-year commercial risk, not a laboratory curiosity
Hydrolysis is the chemical cleavage of a polymer chain by water, and in this industry it is overwhelmingly a polyester-polyurethane problem. The ester linkage in a polyester-based polyurethane is attacked by moisture, the reaction accelerates sharply with temperature, and residual acid from the formulation or from absorbed atmospheric pollution catalyses it further. The symptoms are unmistakable once you have seen them: the coating surface goes tacky, then flakes as a dry powder, the bag develops a faint sweet or musty smell, and eventually the coating separates from the cloth in sheets.
Typical field onset for a mid-grade polyester polyurethane coating is somewhere between three and seven years in a temperate climate, and considerably faster in hot, humid storage. A container sitting in a port in Southeast Asia through a summer, or stock held in a non-climate-controlled warehouse for a year before sale, can move that onset forward by years. Polyether-based polyurethane resists hydrolysis far better but costs more and has lower tensile and abrasion properties, which is why it has never fully displaced the polyester type.
Silicone does not have an ester linkage to cleave. The siloxane backbone is not attacked by water in the same way, which means a silicone-coated fabric does not go tacky in storage and does not have a shelf life governed by humidity. Realistic storage life is measured in decades rather than years, and this is a genuine commercial argument in two specific situations: programmes with long or unpredictable inventory turns, and products sold with a multi-year warranty where year-four claims are the expensive ones.
Two honest caveats. First, the nylon base cloth still ages: it absorbs moisture, it slowly yellows, and it loses strength under prolonged ultraviolet exposure regardless of what is coated on it. Second, and more important, specifying a silicone shell does not make the bag hydrolysis-proof, because the polyurethane-coated zipper tape, the seam sealant, the bonding films on any logos and the internal barrier layer are all still polyurethane. The bag fails at its weakest polymer, and the shell is rarely that polymer.
Silicone versus PU versus TPU: the comparison that actually decides
Quotations for premium waterproof cloth usually resolve to three options, and the decision is not about which is best but about which failure mode you are willing to accept. The table below is written as a decision table: the last column states what the row means for a real programme rather than restating the numbers.
| Decision factor | Silicone-coated nylon | PU-coated nylon or polyester | TPU film laminate | What it means for your programme |
|---|---|---|---|---|
| Hand feel | Dry, slippery, low friction | Slightly rubbery, grippy | Smooth but firmer | Silicone wins where touch sells the product |
| Low-temperature flex | Outstanding to extreme cold | Stiffens and crazes below about minus 20 °C | Good, depending on soft segment | Silicone or polyether TPU for winter and cold-chain |
| Hydrolysis and storage | No ester link; very long life | The main long-term failure mode | Polyether grades good, polyester grades poor | Silicone removes a warranty category entirely |
| Typical water column | 1,000–3,000 mm | 3,000–10,000 mm | 5,000–20,000 mm | Matters only where the bag is compressed under load |
| Weldability | Cannot be heat sealed or RF welded | Welds acceptably with tuned parameters | Welds best of the three | Silicone forces stitched and sealed seams |
| Printability | Poor without pre-treatment | Good with standard inks | Good with PU-based ink systems | Silicone needs plasma, silicone ink or a label |
| Tear per gram | Best of the three | Lowest, because coating locks the yarns | Moderate | Silicone wins lightweight tear-critical designs |
| Abrasion per gram | Weakest against sharp abrasion | Moderate | Best | Concrete, sand and tools argue against silicone |
| Indicative price per metre | 3–7 USD | 1–3.50 USD | 4.50–9 USD | Silicone costs roughly double a standard PU cloth |
Two rows deserve more than a glance. Weldability is the one that changes the whole construction: a silicone-coated shell has to be sewn, and the seam then has to be sealed with a liquid silicone sealant or covered with a tape whose adhesive has been tested against that specific low-energy surface. That is a slower, more labour-intensive process than welding, and it changes the achievable water ingress performance. The trade-offs between the joining routes are set out in our comparison of stitched, welded and bonded construction.
The other row worth pausing on is the hybrid possibility that does not appear in the table at all. A fabric with silicone on the face and polyurethane on the back gives you most of the hand feel and water shedding, plus a weldable inner face. It is frequently the right commercial answer, and the price of it is that the polyurethane back coating reintroduces the hydrolysis risk you were trying to buy out. Ask which side the polyurethane is on and what grade it is.
For a direct head-to-head on the two film-forming options, our separate comparison of TPU and PVC waterproof materials covers the performance and compliance differences in more depth.
Coating weight: the grams per square metre decision
Coating weight is the single most useful number on the specification and the one most often missing from it. It is expressed as dry add-on in grams per square metre, and it has to be stated per side, because a fabric coated on both faces carries roughly double the weight of a single-sided one and behaves differently when wet. Below about 8 grams per square metre per side you are buying a handle treatment rather than a barrier.
| Dry add-on per side | Water column you can expect | Handle and weight penalty | Best application |
|---|---|---|---|
| 3–6 g/m² | Under 500 mm; sheds splash only | Almost none | Handle finish over another barrier layer |
| 8–12 g/m² | Roughly 800–1,200 mm | Very light, packs small | Stuff sacks, pack liners, ultralight rain covers |
| 15–22 g/m² | Roughly 1,200–2,500 mm | Light; the default balance | Dry bags, lightweight backpacks, premium totes |
| 25–35 g/m² | Roughly 2,500–5,000 mm | Noticeably stiffer and heavier | Base panels and high-wear zones on premium product |
| Above 40 g/m² | Diminishing returns | Fold-cracking risk rises fast | Rarely justified; change the base cloth instead |
Coating both faces costs more and adds weight, but it solves a specific problem that single-sided silicone cloth has. Nylon absorbs roughly three to four per cent of its own weight in water and swells when it does, so a bag made from fabric coated only on the inside will wet out on the face, get heavier through the day, and sag. Coating both sides prevents that and it doubles the barrier against slow wetting-through at abrasion points. On a product that will be used in sustained rain it is usually worth the cost; on a dry bag that is submerged briefly and then dried, it is not.
There is also a subtle reason the water column figure understates silicone performance in light duty. Because the surface energy of cured silicone is very low, water beads and runs off rather than wetting the face, so the fabric stays lighter and dries faster than a polyurethane-coated cloth at the same measured rating. That helps enormously against rain and splash, and not at all against sustained pressure, which is precisely why the specification should state the duty rather than chase the number.
Whichever band you choose, write it with a tolerance across the roll width. A coating that averages 18 grams per square metre but varies between 12 and 26 will fail first at the thin stripes, and no average figure will save it. Knife-over-roll and gravure application differ in exactly this respect, and the uniformity question is worth asking at quotation stage. The relationship between coating weight and the measured rating is explained further in our article on hydrostatic head ratings for waterproof fabrics.
Where silicone fights your factory: welding, sewing and printing
This is the section that saves money, because every problem in it is cheap to design around and expensive to discover in bulk. A cured silicone coating is a thermoset. It does not melt, it does not re-flow under heat, and its dielectric loss is too low for radio frequency welding to couple energy into it effectively. A supplier who offers radio-frequency-welded silicone-coated nylon is either using a hybrid fabric or will deliver seams that look acceptable on the line and peel in the field. Ask which it is before sampling, not after.
The four workable routes are these. Stitch and seal with a liquid silicone sealant applied to the needle line, which is slow, operator-dependent and needs a cure window before testing. Stitch and cover with a tape whose adhesive has been peel-tested against the actual production surface, which is faster but has a documented adhesion penalty on low-energy faces. Weld a polyurethane or TPU tape over a stitched seam, giving the strongest result at the highest cost. Or switch the inner face of the fabric to a weldable polymer and weld the construction normally. Each of those is a different price and a different performance level, and all four are covered in principle in our guide to seam taping and sealing methods.
- Sewing: the low-friction face lets plies slide under the presser foot, so expect seam slippage unless a walking foot or compound feed is used and stitch density is raised to around 8 to 10 stitches per inch.
- Needles: silicone builds up on the needle and in the hook, causing skipped stitches and thread breakage. Fine needles of about Nm 70/10, a silicone-compatible lubricant and a defined needle-change interval are standard countermeasures.
- Needle holes: silicone-coated nylon does not swell to close a needle hole the way some coatings do, so every stitch is a potential leak path and seam sealing is not optional.
- Printing: cured silicone has a surface energy around 20 to 24 millinewtons per metre, while most screen inks, heat transfers and films need 38 to 42. Without pre-treatment the print will fail a rub test within weeks.
The print problem has four solutions, and the choice should be made at design stage. Plasma or corona treatment immediately before printing raises the surface energy, but the effect decays within hours to a few days, so treated stock has to be printed immediately and the schedule has to allow for it. Silicone-based inks bond properly but cost more, cure at high temperature and offer a narrower colour range. A polyurethane-coated woven patch or a heat-applied badge bonded with a primer sidesteps the problem entirely and is the usual commercial answer. Embroidery is the worst option: every needle puncture is a leak path that then has to be sealed from the inside. Our overview of logo printing and embroidery options covers the adhesion testing that should accompany whichever route is chosen.
One rule follows from all of this and belongs on the purchase order: any change of coating chemistry or coating weight after sampling invalidates the seam parameters agreed during sampling. Weld settings, needle size, thread tension and print pre-treatment are all calibrated to a specific surface, and a like-for-like substitution is not like-for-like. Re-validation costs days; a field failure costs the programme.
What the water column number hides
Silicone-coated nylon typically reports a lower hydrostatic head than a comparable polyurethane cloth, and buyers reject it on that basis more often than on price. The number is real and it is also widely misread. The standard test clamps a flat specimen and raises a water column until penetration occurs at three points; it measures a specific, artificial condition. What a bag actually experiences is either a brief submersion, sustained rain and splash, or localised compression, and these are different physical situations.
Against rain and splash, silicone performs better than its rating suggests, for the reason given earlier: water never wets the face, so the fabric does not absorb, gain weight or conduct heat away from the contents. Against compression, the rating matters a great deal. A dry bag rolled shut and strapped down, a pack sat on in a vehicle, a bag under a buckle or a hip belt, all generate local pressures equivalent to several thousand millimetres of water column. If your product will be squeezed, the number counts, and a 1,500 mm silicone cloth is genuinely marginal in that spot.
The right specification therefore has three numbers rather than one. Fresh hydrostatic head, which is the least informative of the three and the only one usually quoted. Hydrostatic head after a defined flex or abrasion preconditioning, which is what predicts the fold failures. And a spray or shower test, which is what predicts rain performance. A supplier who can produce all three is describing a material; a supplier who produces one is describing a datasheet.
There is one more place the rating misleads, and it is specific to coated woven cloth. The measured head is often governed by the coating film bridging the gaps between warp and weft at the interlacing points rather than by the barrier properties of the film itself. Raising the coating weight improves the rating largely by thickening those bridges, which is why the number climbs faster than real-world performance does. Test protocols and their interpretation are covered in our piece on seam integrity testing methods and the broader review of waterproof testing standards.
Tear and abrasion: the trade-off that decides whether it belongs on your product
Here is the counterintuitive part, and it is the strongest technical argument for silicone in lightweight construction. When a tear propagates through a coated woven fabric, the yarns at the tear tip either move, bunch and share the load, or they are held rigidly in place and break one at a time. Polyurethane, being a relatively stiff film bonded tightly to the cloth, locks the yarns and produces the second behaviour, which is why a polyurethane-coated fabric often has lower tear strength than the uncoated base cloth. Silicone, being soft and elastomeric, lets the yarns move and produces the first. A 30 denier silicone-coated ripstop can beat a 70 denier polyurethane-coated cloth on a tongue tear test.
Abrasion is the mirror image. Silicone is soft, has a low durometer, and offers little resistance to sharp or particle abrasion. Dragged across concrete, packed with tools, or used on a beach where quartz sand is harder than the coating, it wears through quickly, and because the coating is thin the base cloth is exposed early. Polyurethane and especially a TPU film face outperform it substantially in the same duty.
So the decision rule is a clean one. Silicone buys you tear strength, cold flexibility, storage life and hand feel per gram, and it costs you abrasion life, weldability and printability. It is the right choice where the bag is light, packed soft and handled gently: ultralight dry bags, stuff sacks, pack liners, compression sacks, premium soft totes, lightweight rain covers. It is the wrong choice where the bag is dragged, loaded with hard objects, or used on abrasive surfaces. Denier interacts with all of this, and our article on denier ratings and durability explains how much of the abrasion performance can be bought back by moving the base cloth up rather than the coating.
One design response is worth knowing about because it costs almost nothing: zone the material. Use silicone-coated cloth on the upper panels where weight and feel matter, and a polyurethane or TPU-faced cloth on the base panel and the lower back panel where abrasion concentrates. On a backpack this typically means two fabric codes instead of one and no meaningful cost increase, and it removes the trade-off rather than compromising within it. The same logic is applied to finishes in our review of abrasion-resistant coatings for bag exteriors.
Price bands, minimums and what you are actually paying for
Silicone-coated cloth costs roughly twice what a standard polyurethane-coated cloth of comparable denier costs per metre, and the premium buys longevity and feel rather than raw strength. That is a defensible trade in a premium programme and a poor one in a price-led one, so the honest first question is whether your customer will ever handle the bag before buying it.
| Material | Indicative price per metre | Effect on a 30 litre pack | Ordering constraint |
|---|---|---|---|
| PU-coated 210–420D polyester | 1.00–2.20 USD | Baseline | Usually available from stock in common colours |
| PU-coated 420–600D nylon | 1.80–3.50 USD | Plus roughly 0.60–1.50 USD | Stock colours widely available |
| Silicone-coated 30–70D nylon | 3.00–6.00 USD | Shell weight drops 200–350 g | Custom coating usually needs a roll-lot minimum |
| Silicone-coated 210–420D nylon | 3.50–7.00 USD | Plus roughly 1.50–3.00 USD | Limited colour range; custom colour adds lead time |
| Silicone face, PU back hybrid | 3.00–5.50 USD | Plus roughly 1.20–2.40 USD | Weldable; reintroduces some hydrolysis risk |
| TPU film laminate 0.15–0.30 mm | 4.50–9.00 USD | Plus roughly 2.50–5.00 USD | Film thickness drives both price and stiffness |
The ordering constraint column is the one that causes scheduling trouble. Because the coating is applied to the cloth before cutting and the cloth is bought in roll lots, a custom silicone specification generally carries a fabric minimum measured in hundreds to a couple of thousand metres per colour, which frequently exceeds the bag-level minimum of 500 pieces per style. In practice this means the fabric decision has to be locked before the fabric order is placed, and changing it mid-programme is expensive or impossible. Plan the coating at sampling, not at reorder.
Colour availability is the second practical constraint. Silicone coating lines run a narrower standard colour range than polyurethane lines, and a custom colour usually means a minimum quantity and additional lead time rather than a simple surcharge. If your programme depends on a brand colour, resolve it at the same time as the coating weight, not afterwards.
Buyers selling into the European Union should also confirm the coating supplier’s position on cyclic siloxanes, which are restricted under REACH and tracked by the European Chemicals Agency. A cured silicone coating is not the same substance class as the volatile cyclic siloxanes used in some formulations and finishes, but the question has to be asked of the specific product and answered in writing, because the answer varies between suppliers.
When silicone-coated nylon is the wrong choice
It is worth stating the exclusions plainly, because the material is over-specified almost as often as it is under-specified. A buyer who copies a premium spec onto a work bag inherits the cost without the benefit, and a buyer who specifies it on a product that must be welded creates a production problem rather than solving one.
- Heavy abrasion duty: dragging, concrete, tools, sand. Use a TPU film face or a heavier polyurethane-coated cloth and accept the weight.
- Constructions that must be welded to reach a submersion rating: silicone cannot be welded, so the seam design has to change or the material has to change.
- Complex multicolour decoration: low surface energy defeats most ink systems, and the workaround costs more than the coating saves.
- Price-led programmes: the premium buys longevity and feel, and neither is visible on a shelf where the customer cannot touch the product.
- Recyclability claims: a silicone-coated nylon is a mixed-polymer laminate that most recycling streams cannot separate, which undercuts end-of-life messaging.
- High-load carrying with hard contents: soft coating and light denier give poor puncture resistance.
- Very short product life expectations: if the bag is expected to last one season, the hydrolysis advantage is never realised.
The pattern behind all seven is that silicone pays back over time and through touch. Where neither of those is part of the value proposition, the money belongs in denier, in construction or in finishing instead. Our discussion of lightweight material optimisation approaches the same trade from the other direction, starting from the weight target rather than from the coating.
How to write silicone-coated nylon into a tech pack
Everything above compresses into lines that can be quoted against. Written this way, the coating stops being a conversation about feel and becomes a requirement that a supplier can price and a laboratory can verify.
- Base cloth: denier, nylon 6 or 6.6, weave type, ripstop grid spacing, filament count, and the supplier or grade if you have one.
- Coating chemistry: silicone elastomer, plus the cure type. State explicitly whether any polyurethane or TPU layer is present and on which face.
- Add-on: dry grams per square metre per side, with a tolerance across the roll width, not a target average.
- Hydrostatic head: fresh, plus after a defined flex or abrasion preconditioning, plus a spray test result. Three numbers.
- Cold performance: minimum service temperature, cold bend temperature and mandrel diameter, and a post-fold water column retest.
- Seam construction: stitch type, stitches per inch, thread, sealant chemistry or tape specification, and the peel strength target measured on the production surface.
- Decoration: method, pre-treatment with a stated surface energy target in millinewtons per metre, and a rub fastness requirement.
- Abrasion: method, abradant, load, cycles and endpoint, run wet wherever the product meets water.
- Compliance: REACH and siloxane statement, plus any restricted substance testing required by the destination market.
- Change control: a line stating that any change of coating chemistry or weight invalidates the agreed seam and print parameters.
The last line is the one buyers omit and later wish they had not. Coating substitution happens for supply reasons rather than technical ones, and it is frequently presented as equivalent. With the line in place, a substitution triggers re-validation and the cost is visible; without it, the change happens silently and the failure appears in the field.
Ultraviolet behaviour is the remaining property worth specifying, because silicone-coated nylon is often chosen precisely for outdoor products. Cured silicone is far more UV-stable than polyurethane and does not yellow the way polyurethane coatings do, but the nylon underneath still loses strength under prolonged exposure and any dyestuff still fades. Our article on UV resistance in outdoor bag materials sets out what to require, and the accelerated protocols that predict it are described in our piece on accelerated ageing tests.
Sampling and validation before you commit to bulk
A silicone specification is more sensitive to process detail than a polyurethane one, so the sampling stage has to carry more of the validation load. The tests that matter are not the ones on the material datasheet, which describe the cloth, but the ones on the finished construction, which describe the bag.
- Seam peel strength measured on the actual production surface with the actual sealant or tape, not on bare fabric.
- Cold bend at the specified temperature followed by a water column retest on the folded region.
- Hydrostatic head after a defined abrasion preconditioning, to catch the fold and wear failure modes.
- Print cross-hatch and rub fastness run on the production ink and the production surface together.
- Fill, hang and invert test on a finished sample, because closure geometry defeats more waterproof bags than fabric does.
- Heat ageing, typically around 70 degrees Celsius for a week, as a proxy for storage and transport conditions.
Sequencing matters. Because the coating may need to be ordered in a roll lot and because the seam and print parameters have to be developed against the specific surface, the coating choice has to be made at the start of sampling rather than at the end of it. A programme that samples a polyurethane cloth and then asks for silicone in the same design is effectively restarting the engineering, and the lead time moves with it. What to expect from that stage is described in our guide to custom waterproof bag sampling, and where the material money sits in the finished quotation is laid out in our breakdown of custom waterproof bag cost.
If you want this applied to a specific style, send the duty description, the artwork and the target price and let the coating be proposed against the duty rather than chosen from a swatch book — the two often give different answers. Every style starts at 500 pieces minimum, with samples in 6–10 working days and bulk in 35–50 days, quoted FOB Xiamen.
Frequently Asked Questions
Q1. What is silicone-coated nylon?
A nylon base cloth, usually ripstop, carrying a crosslinked silicone elastomer coating instead of polyurethane. Typical coating weight is 10 to 35 grams per square metre per side, cured at 150 to 180 degrees Celsius into a thermoset rubber that does not melt again.
Q2. Is silicone-coated nylon more waterproof than PU-coated fabric?
Usually not by the laboratory number. Silicone typically reports 1,000 to 3,000 millimetres of water column against 3,000 to 10,000 for polyurethane. It performs better than its rating in rain because water never wets the face, and worse under sustained compression.
Q3. Why is silicone-coated nylon more expensive?
The coating chemistry costs more and the application is slower, typically doubling the price per metre. What you buy with it is cold flexibility, resistance to hydrolysis, ultraviolet stability and a measurably better hand feel.
Q4. Can silicone-coated nylon be welded?
No. Cured silicone is a thermoset and does not melt or re-flow, and it does not couple effectively with radio frequency energy. Silicone shells are stitched and then sealed with liquid silicone sealant, taped, or built from a hybrid fabric with a weldable inner face.
Q5. Why does print peel off silicone-coated fabric?
Cured silicone has a surface energy of about 20 to 24 millinewtons per metre, while most inks and transfer films need 38 to 42. Solutions are plasma or corona pre-treatment immediately before printing, silicone-based inks, or printing onto a polyurethane-coated patch.
Q6. What is the difference between a silicone coating and a silicone finish?
A coating is 10 to 35 grams per square metre and is a waterproof barrier. A finish is 2 to 5 grams per square metre, changes the hand feel and sheds water, but will not hold a water column. Both are sold as silicone.
Q7. How long does silicone-coated nylon last in storage?
Far longer than polyurethane-coated cloth. Silicone has no ester linkage for water to cleave, so it does not go tacky or flake in humid storage. Realistic life is measured in decades, though the nylon base and any polyurethane components still age.
Q8. What causes polyurethane coatings to go sticky and flake?
Hydrolysis. Moisture cleaves the ester links in a polyester-based polyurethane, accelerated by heat and residual acid. Typical field onset is three to seven years in a temperate climate and much faster in hot, humid storage.
Q9. Is silicone-coated nylon better in cold weather?
Yes, substantially. Its glass transition is around minus 120 degrees Celsius, so it stays flexible at temperatures where polyurethane stiffens and crazes at folds, typically somewhere between minus 15 and minus 30 degrees Celsius.
Q10. Does silicone-coated nylon abrade well?
No. The coating is soft and thin, so it wears through quickly against sand, concrete or sharp contents. It has excellent tear strength for its weight, which is a different property, and the two are often confused.
Q11. Why does silicone fabric have better tear strength than PU fabric?
Because the soft elastomeric coating lets yarns move and bunch at the tear tip so they share the load. A stiff polyurethane film locks the yarns in place so they break one at a time, which is why coating sometimes lowers tear strength.
Q12. How much coating weight do I need?
Around 15 to 22 grams per square metre per side is the default balance for bags, giving roughly 1,200 to 2,500 millimetres of water column. Below about 8 grams you have a handle finish rather than a barrier, and above 40 grams fold cracking becomes the limiting problem.
Q13. Should the fabric be coated on both sides?
For sustained wet duty, yes. Nylon absorbs three to four per cent of its weight in water and sags when it does, so a single-sided fabric wets out on the face and gets heavy. For brief submersion followed by drying, one side is enough.
Q14. Can I change the coating after sampling?
Not cheaply. Seam parameters, needle selection and print pre-treatment are all calibrated to a specific surface, so a coating change invalidates them. It also usually triggers a fabric roll-lot minimum that exceeds the bag-level minimum quantity.
Q15. What coating weight tolerance should I specify?
State a tolerance across the roll width rather than a target average. A coating averaging 18 grams but varying between 12 and 26 will fail first at the thin stripes, and the average figure will not reveal that.
Q16. Is silicone-coated nylon recyclable?
Not easily. It is a mixed-polymer laminate that most mechanical recycling streams cannot separate, which matters if the programme carries end-of-life or recycled-content claims. Check this against your sustainability messaging before committing.
Q17. What tests should I run on a silicone-coated sample?
Seam peel on the production surface, cold bend followed by a water column retest on the fold, hydrostatic head after abrasion preconditioning, print rub fastness on the production ink, and a fill-and-invert test on a finished bag.
People Also Ask
What is silicone-coated nylon used for?
Ultralight and premium waterproof products: dry bags, stuff sacks, pack liners, compression sacks, lightweight shells and soft totes where weight, hand feel and long storage life matter more than abrasion.
Is silnylon more waterproof than PU-coated nylon?
Usually not by the measured water column. It performs better in rain because water beads and runs off, and worse under sustained compression, so the duty decides which matters.
Why can silicone-coated fabric not be welded?
Because cured silicone is a thermoset. It does not melt or re-flow under heat, and it does not absorb radio frequency energy, so seams must be stitched and sealed instead.
How do you print on silicone-coated nylon?
Raise the surface energy first with plasma or corona treatment, use silicone-based inks, or print onto a polyurethane-coated patch. Standard screen inks fail a rub test within weeks.
Does silicone coating last longer than polyurethane?
Yes. It does not hydrolyse, so it stays flexible and non-tacky in humid storage for decades, while polyester polyurethane typically begins to degrade within three to seven years.
What coating weight is right for a dry bag?
Around 15 to 22 grams per square metre per side, giving roughly 1,200 to 2,500 millimetres of water column. Lighter for stuff sacks, heavier only on high-wear panels.