RF welding and hot-air welding are the two production routes that make a waterproof seam truly waterproof, and they differ in how they deliver heat, what materials they join, and what programs they price: RF welding excites the polymer itself with radio-frequency energy for precise, uniform seams on TPU and PVC laminates, while hot-air welding blows controlled heat into the seam zone and follows curves, thick materials and large formats that RF presses cannot hold — so the route decision follows material, geometry and volume, and a program that picks the wrong route pays in seam defects, tooling costs or both. This guide compares the two methods on seam physics, material compatibility, speed and tooling economics, and production quality control, and closes with the decision table that routes a custom waterproof bag program to the right machine — at MOQ 500 quantities where the choice affects unit cost, delivery and the seam warranty the buyer can actually underwrite.
Working reference: QUANZHOU JUNYUAN BAGS, custom waterproof bag production since 2014 from a 4,950 m² SGS-verified facility running 7 lines, 149 machines and 137 staff at 200,000 pieces monthly. MOQ 500 per design, samples 6–10 working days, bulk 35–50 days, AQL 2.5 inspection, 30/70 T/T, FOB Xiamen, shipping to 100+ countries.
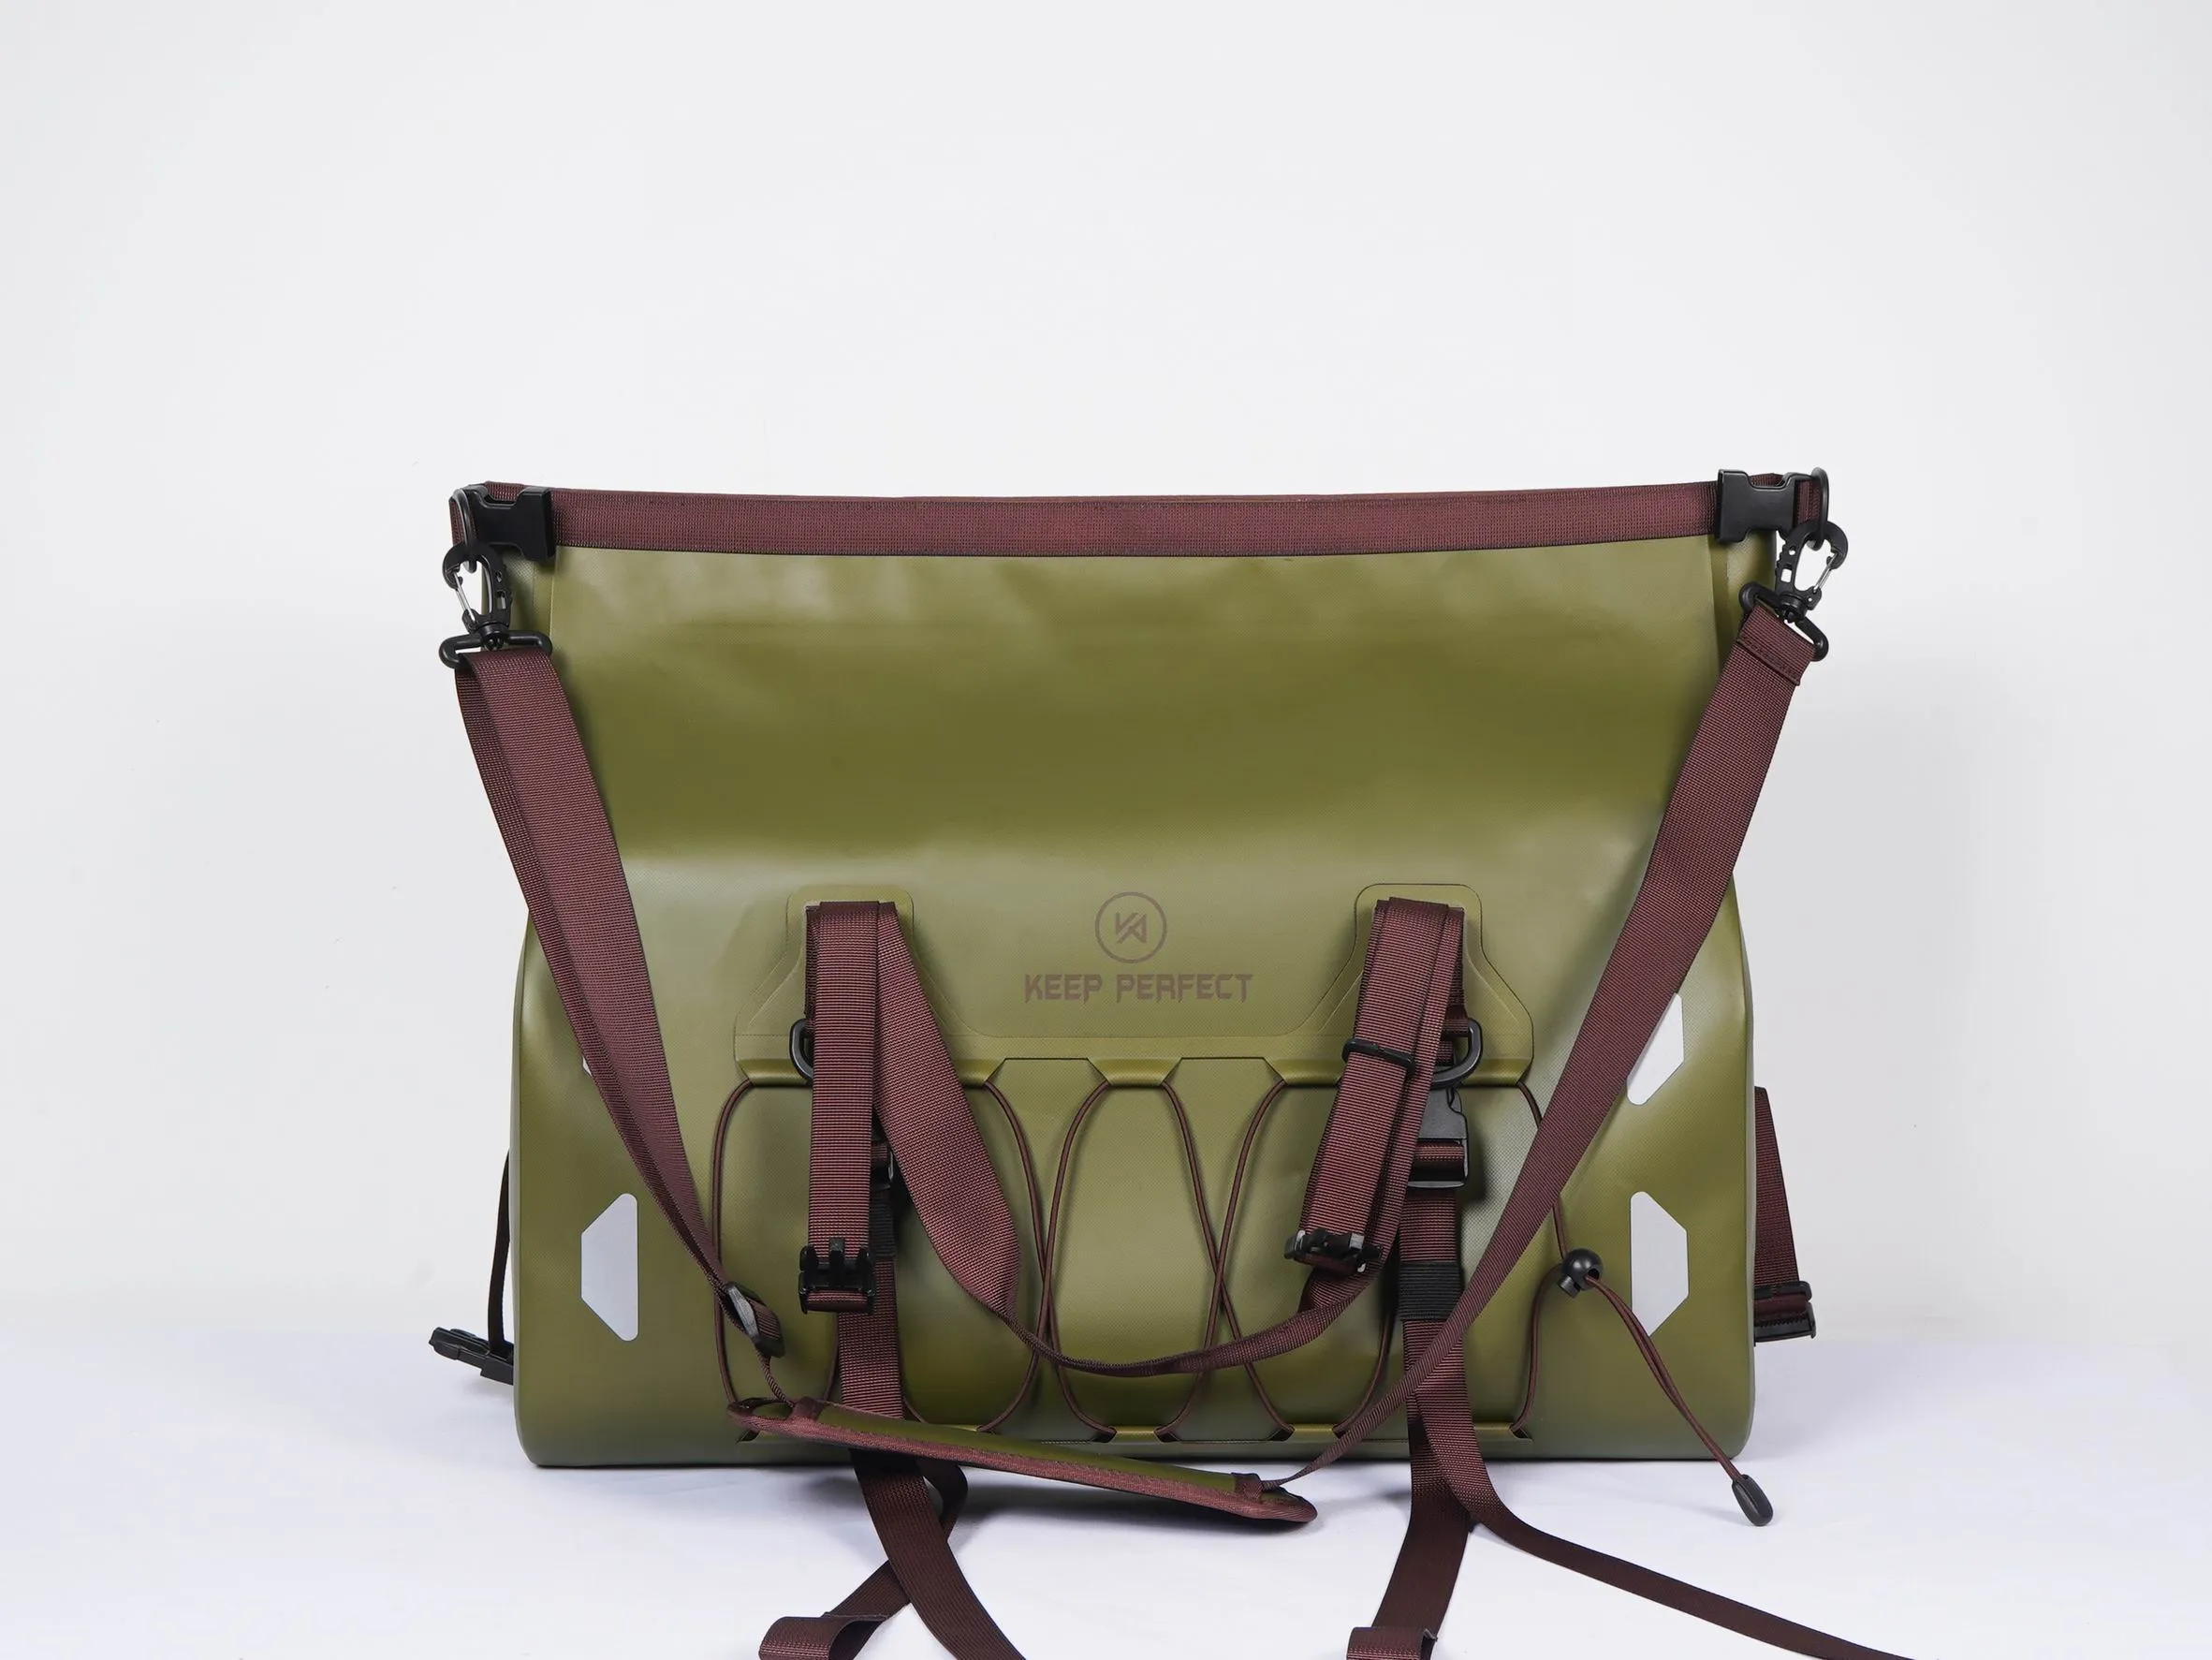
Two ways to make one polymer
Both methods reach the same destination — two pieces of coated or laminated fabric fused into a continuous polymer joint with no stitch holes to leak — but they travel by different physics. RF (radio-frequency) welding, the same technology as high-frequency welding, applies an alternating electric field to the seam zone through a die: polar polymers in the film attempt to re-orient with each field reversal, and the internal friction of millions of re-orientations per second heats the weld zone from the inside out. The die presses the molten zone flat, the field stops, and the joint cools under pressure into a seam that is chemically continuous. Hot-air welding heats from the outside in: a nozzle delivers precisely controlled hot air into the seam gap while a roller presses the softened polymers together, following the seam path like a sewing machine follows a stitch line. The distinction that drives everything downstream: RF heats only what the field touches and needs a press that physically clamps the whole seam at once, while hot-air heats a moving zone and needs an operator or fixture that guides the nozzle. That single difference — batch press versus continuous path — explains the tooling costs, the geometry limits, the speed figures and the seam characters that make the two routes right for different programs. The process itself, die by die and parameter by parameter, is documented in our high-frequency welding process guide.
Material compatibility: the first gate
The route decision is half-made before any machine runs, because the materials decide what can be welded at all. RF energy couples with polar polymers: PVC and TPU films respond strongly, which is why the welded waterproof bag industry standardized on them — the film choices our TPU thickness guide maps gauge by gauge, and the material trade-offs in our TPU versus PVC comparison. Polyethylene and polypropylene are non-polar and barely respond to the RF field, so laminates built on PE films weld hot-air or not at all. Hot-air is the material-agnostic route: it heats any thermoplastic that softens and fuses, including the PE and PP laminates RF cannot excite, thick dual-coated fabrics, and heavy industrial materials that exceed RF press depth. The compatibility table is therefore the first page of the decision: a TPU-laminated dry bag can go either route; a PE-laminated utility cover has one route; a program unsure of its laminate should decide its film before its machine.
| Material system | RF welding | Hot-air welding | Notes |
|---|---|---|---|
| TPU-laminated polyester/nylon | Excellent — the standard route | Excellent | TPU responds to RF and fuses cleanly hot-air |
| PVC-coated fabrics | Excellent — legacy standard | Good | PVC couples strongly; phthalate rules push to TPU |
| PE/PP laminates | No — non-polar, field will not couple | Good — the viable route | Utility covers, tarps, PE films |
| Heavy dual-coated fabrics | Press-depth limits | Excellent — no depth limit | Industrial curtains, containment builds |
| EVA films | Marginal — weak coupling | Good | EVA usually routes to hot-air or heat sealing |
Seam character: what the weld looks and behaves like
The two routes leave recognizable fingerprints on the finished seam, and buyers can read them. An RF weld is typically a pressed, uniform 8–10 mm seam with a die-marked edge texture — flat, consistent, and visually clean because the die pressed the whole seam at once under identical conditions. A hot-air weld is a slightly narrower, more flexible seam — commonly 6–8 mm — with a hand-guided character that skilled operators keep remarkably uniform but that carries the natural micro-variance of a moving process. The behavioral consequences follow the character: RF’s die-pressed uniformity gives seam strength consistency that suits rating-critical builds — the seam integrity verification our seam testing guide documents — while hot-air’s narrower, softer seam flexes more at fold lines and follows curved edges, gussets and three-dimensional corners that a flat RF die cannot wrap. Neither character is superior; they serve different geometries, and the strongest programs use both on the same bag where geometry demands it: RF for the long flat panels, hot-air for the curved attachments.
Geometry and format: what each machine can reach
The physical machine sets hard limits the spec sheet must respect. An RF weld happens inside a press between two electrodes, so the seam must fit within the press bed and lie flat under the die: long straight panels, circumferences under the bed size, and repetitive small parts are RF’s natural territory — dry bag bodies, tote side seams, pouch perimeters. Three-dimensional assemblies, very large circumferences, attached tubing, field-repair-scale odd shapes and on-material joins onto existing structures exceed the press and belong to hot-air, whose nozzle goes anywhere a hand and fixture can. The format logic repeats across the industry: the welded dry bag standard — 500D TPU-laminated polyester, the build class our dry bag sizing guide documents — is an RF product because its geometry is a rolled cylinder of flat panels; boat covers, containment berms and curtain-wall builds are hot-air products because their geometry is assembled in place at scale. A buyer reviewing a welded quotation should ask which seams run which route, because the answer reveals whether the factory engineered the geometry or fought it.
Speed, tooling and the economics of scale
The cost structure differs at the tooling line. RF welding needs a die per seam pattern — a machined brass or aluminum electrode cut to the seam’s shape, amortized across the program’s whole production life. That die cost is why RF loves repetition: the first unit carries the tooling, the next ten thousand carry almost none. Cycle time per weld is seconds-to-tens-of-seconds in the press, and multi-station dies weld whole perimeters in one press cycle, which is how high-volume dry bag lines hit their output numbers. Hot-air welding needs no per-program die — the nozzle and roller follow any path — so its entry cost is near zero and its per-unit economics depend on operator pace rather than press cycles. The crossover is predictable: high-volume, repeating geometries amortize RF tooling into lower unit costs; short runs, prototypes and non-repeating shapes favor hot-air’s zero tooling. At MOQ 500, most programs sit in RF’s sweet spot — tooling amortizes across the run while press cycles deliver consistency a moving nozzle cannot — and mixed programs split routes by seam, not by bag.
| Economic factor | RF welding | Hot-air welding |
|---|---|---|
| Tooling per program | Die required, $200–$2,000 by complexity | None — nozzle follows any path |
| Unit time driver | Press cycle (seconds per multi-seam hit) | Operator pace along the path |
| Volume behavior | Unit cost falls as tooling amortizes | Unit cost flat across volumes |
| Best program fit | 500+ repeating units, flat geometries | Short runs, curves, assemblies, repairs |
| Skill dependency | Die quality + press parameters | Operator skill — the seam is handmade |
Quality control: how each route fails and how to catch it
Both routes fail in characteristic ways, and the inspection protocol should aim at each method’s known weak points. RF welds fail at the edges: under-welding from low energy or short cycles leaves a seam that looks pressed but fuses shallow; arcing — a die-to-material spark — burns pinholes into the film; and die wear degrades edge pressure gradually, which is why production lines re-verify die condition on schedule. Hot-air welds fail along the path: heat and speed variance leaves cold or cooked segments, the start-stop points of each pass are the classic weak links, and operator fatigue shows up as micro-variance long before it shows up as failure. The verification toolkit is shared and cheap: the towel-and-submersion protocol from our testing guide catches any seam leak in thirty minutes; peel testing of sample welds — pulling a welded strip apart to observe fusion — is the destructive check that reveals shallow fusion; and pressure testing inflated welds exposes pinholes the eye cannot. AQL 2.5 bulk inspection — the acceptance discipline our AQL buyers guide documents — pulls samples per lot and runs them through the same protocol, so the route’s failure mode is caught at the dock, not in the field. Peel and seam-strength figures are comparable between two suppliers only when the method is named with its edition — the standard test methods the industry cites are published by ASTM International, and the method number belongs on the purchase order beside the result.
The ultrasonic and heat-sealing alternatives
Two further methods bracket the comparison and deserve their seat at the table. Ultrasonic welding generates heat mechanically — a horn vibrates the materials at ultrasonic frequency and interfacial friction does the fusing — which makes it the precision route for thin films, sealed cuts and high-speed discrete parts, the comparisons our heat-sealing versus ultrasonic guide maps in detail. Heat sealing — the simple hot-bar route — is the economy entry for straight seams in compatible films. In the route family, RF and hot-air remain the load-bearing pair for bag bodies because they carry the seam widths, material ranges and geometries bags actually have, while ultrasonic serves where precision and speed outweigh width, and hot-bar serves where straightness is guaranteed. The full stitched-taped-bonded decision landscape — including when sewn construction beats welding — is documented in our construction methods comparison, and the sewn route’s own sealing methods in our seam taping guide.
Sustainability and the PVC question
Route choice touches the materials debate. RF welding’s strongest coupling polymer is PVC — legacy, cheap, and increasingly regulated for phthalate plasticizers in consumer markets, the regulatory pressure our PVC-free alternatives guide documents. The industry’s answer has been TPU: it couples well for RF, is PVC-free, and carries the environmental story programs increasingly need — including the recycled-content variants our recycled TPU guide covers. The route decision is therefore also a positioning decision: a TPU-laminated RF-welded build is simultaneously the engineering choice and the compliant, marketable one. Hot-air shares the same material logic with one addition — its PE and PP compatibility keeps single-polymer, mono-material constructions weldable, which matters for recyclability targets, the end-of-life considerations our end-of-life guide raises. Buyers with sustainability commitments should hand their certification requirements to the supplier at quotation, because film selection and route selection resolve together. The restriction list behind that regulatory pressure is the REACH framework maintained by the European Chemicals Agency, and it moves faster than most product calendars.
Specifying the route on a purchase order
A route-specified purchase order names four lines. The seam construction line: which seams weld, by which method, at what width — “RF-welded, 8–10 mm, all body seams; hot-air, 6–8 mm, handle attachments” is a complete sentence. The material line: the laminate system the route depends on — “500D polyester, TPU film, 0.25 mm gauge” — the film spec our TPU guide standardizes. The verification line: peel tests on start-of-run samples, submersion or pressure tests per the testing protocol, and AQL 2.5 on bulk. And the tooling line: who owns the RF die, what it costs, and that it stores for reorders — the reorder economics our reorder process guide documents, since stored tooling is what makes a reorder a two-week event instead of a re-tooling project. Orders written that way do not generate seam disputes, because the buyer and factory signed the same physics before production; the full production chain is documented.
The decision table: routing a program in one look
Every factor above compresses into the table buyers keep, and its use is simple: find the row that describes the program and read the route. The rows deliberately overlap, because real programs mix — and mixed programs split routes by seam, which is the last row’s lesson.
| Program profile | Route | Why |
|---|---|---|
| TPU dry bags, repeating geometry, 500+ units | RF welding | Tooling amortizes; press-cycled uniformity at rating-critical seams |
| Curved attachments, 3D assemblies, gussets | Hot-air welding | Nozzle follows geometry a press cannot hold |
| PE/PP laminates, utility formats | Hot-air welding | Non-polar films do not couple to the RF field |
| Heavy industrial materials, thick builds | Hot-air welding | No press-depth limit; fuses at any thickness |
| Mixed-geometry bag family, one calendar | Both, split by seam | RF flats, hot-air curves — engineered, not fought |
| Prototype or short run before tooling | Hot-air first | Zero tooling proves the design; RF follows at volume |
The route decision is the first engineering conversation of a welded program, and it deserves to happen before the quotation rather than during production. Buyers who arrive with the material system named, the geometry mapped and the seam table sketched get 24–48 hour quotations that hold, golden samples in 6–10 working days that match, and bulk at AQL 2.5 that passes — because the machine that made the sample is the machine that makes the bulk, and both were chosen for the program on purpose.
Frequently Asked Questions
Q1. What is the difference between RF welding and hot-air welding?
RF welding heats the seam from inside using radio-frequency energy in a press; hot-air welding heats from outside with a controlled air stream along a moving path. RF suits flat repeating seams in polar films; hot-air suits curves, thick materials and any thermoplastic.
Q2. Which welding method is stronger for waterproof bags?
Both produce seams exceeding the fabric’s strength when done correctly. RF offers die-pressed uniformity for rating-critical flat seams; hot-air offers narrower, more flexible seams and reaches geometry RF cannot.
Q3. Can TPU fabric be RF welded?
Yes — TPU is polar and couples well with RF energy; TPU-laminated polyester is the industry-standard RF-welded construction for dry bags and submersion-grade builds.
Q4. Can PE or PP fabrics be RF welded?
No — polyethylene and polypropylene are non-polar and barely respond to the RF field. They weld by hot-air or heat-sealing routes instead.
Q5. Why does RF welding need a die?
The die is both electrode and press tool: it concentrates the RF field along the seam shape and clamps the weld zone flat. Each seam pattern needs its own die, which is why RF economics favor repeating production.
Q6. How wide is a welded seam?
Typically 8–10 mm for RF die-pressed seams and 6–8 mm for hot-air welds. Width is specifiable and should appear on the purchase order beside the method.
Q7. Is hot-air welding slower than RF welding?
Per seam, usually yes: hot-air runs at operator pace along the path while RF presses whole seams in seconds. At volume with repeating geometry, RF outproduces hot-air decisively.
Q8. Which method costs less for a short production run?
Hot-air: it needs no per-program tooling, while RF requires a die. At MOQ 500 and above with repeating seams, RF tooling amortizes and its unit economics win.
Q9. Can one bag use both welding methods?
Yes, and engineered bags do: RF for the long flat body seams, hot-air for curved attachments, gussets and hardware joins where the press cannot reach.
Q10. How do I test a welded seam before bulk?
Peel-test sample welds for fusion depth, run the towel-and-submersion protocol for leaks, and pressure-test inflated seams for pinholes — then hold bulk to AQL 2.5 on the same protocol.
Q11. What causes RF weld failures?
Edge and energy problems: under-welding from low power or short cycles, arcing pinholes from die contamination, and gradual die wear — all caught by scheduled die checks and peel tests.
Q12. What causes hot-air weld failures?
Path variance: cold or cooked segments from heat/speed drift, and the start-stop joints of each pass — the classic weak links, caught by continuous-path inspection.
Q13. Is RF welding the same as high-frequency welding?
Yes — RF (radio frequency) and HF (high frequency) welding are the same technology; the terms are interchangeable across the industry.
Q14. Which route is more sustainable?
Route follows film: TPU laminates are PVC-free and RF-weldable, making TPU-plus-RF the compliant standard; hot-air additionally welds mono-material PE/PP builds that aid recyclability.
Q15. How much does RF tooling cost?
A program die typically runs $200–$2,000 depending on seam complexity — amortized across the production life, stored for reorders, and usually quoted separately from unit price.
Q16. Which route should a dry bag program use?
RF welding: the dry bag is a rolled cylinder of flat seams in TPU laminate — repeating geometry, polar film, 500+ units — the textbook RF profile the whole category runs on.
People Also Ask
What does RF welding mean?
Radio-frequency welding: an alternating electric field heats polar films from the inside, pressed flat by a shaped die until fused — producing uniform, stitch-free seams in TPU and PVC laminates.
Is RF welding waterproof?
A correct RF weld is a continuous polymer joint with no needle path — as waterproof as the film itself, and verified by submersion and pressure testing before bulk release.
What materials can be hot-air welded?
Any thermoplastic that softens and fuses: TPU, PVC, PE, PP and EVA laminates — including the non-polar films RF cannot couple, and heavy fabrics beyond press depth.
How strong is a welded seam?
When correctly fused, the weld exceeds the surrounding fabric — failures move to the material, not the joint. Fusion depth is verified by peel-testing sample welds.
Why is welding better than sewing for waterproof bags?
Sewing punches needle holes — a permanent leak path. Welding fuses the films into one continuous polymer, which is why submersion-grade builds are welded, never stitched.
What is a hot-air welder used for?
Sealed seams along moving paths: curved attachments, three-dimensional assemblies, industrial curtains and containment builds, plus PE/PP laminates that will not RF weld.